
HomecapabilitiesChemistries
Chemistries
Overview
Cohizon Life Sciences offers extensive expertise across specialized reaction chemistries for agrochemical, specialty chemical, and non-GMP pharmaceutical applications. Backed by advanced process understanding, dedicated infrastructure, and strong safety systems, our capabilities span lab, pilot, and commercial-scale manufacturing with a strong focus on scalability, process efficiency, solvent recovery, and safe handling of complex chemistries.
Core Chemistries
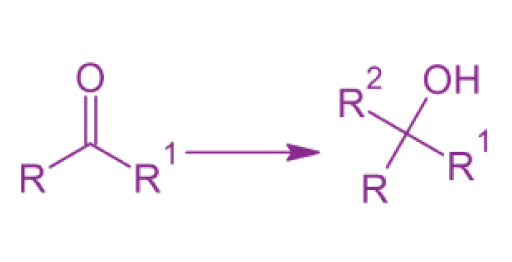
Grignard Reaction
Controlled organometallic synthesis with expertise in process safety, peroxide checks, and solvent recovery for scalable manufacturing applications.
Friedel-Crafts Reaction
Commercial-scale alkylation and acylation capabilities using catalysts including AlCl₃, supported by efficient effluent handling and by-product recovery systems. Scale: 1000 MT Year: 2006
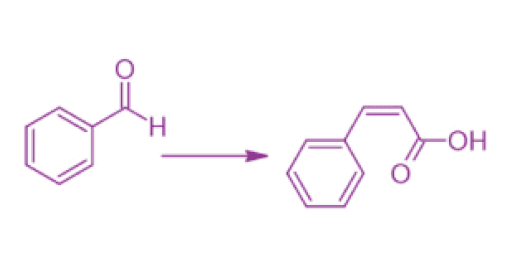
Perkin Reaction
Capabilities for manufacturing α,β-unsaturated aromatic acids and α-substituted β-aryl acrylic acids with commercial-scale salt recovery and recycling systems.
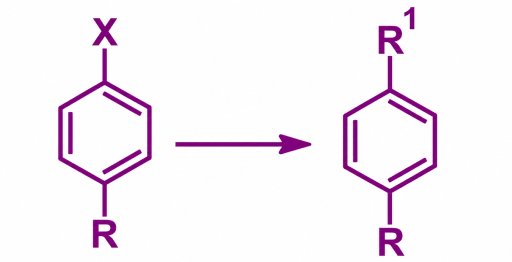
Suzuki & Coupling Reactions
Expertise in boronic acid generation, precious metal recovery, and scalable coupling reactions for complex chemical synthesis. Scale: 700 MT Year: 2003
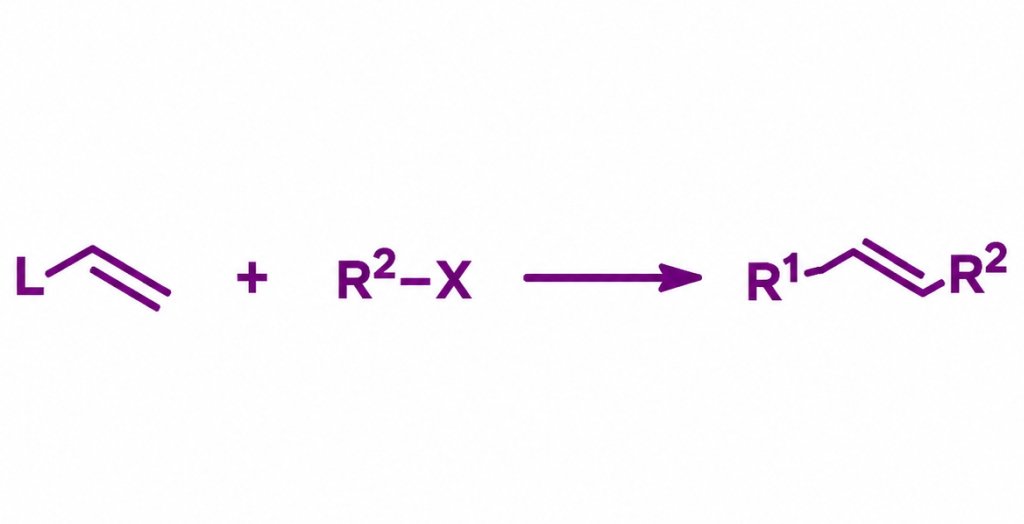
Heck Carbonylation
High-pressure and high-temperature carbonylation capabilities using precious metal catalysts for carboxylic acid and derivative synthesis.
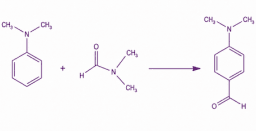
Vilsmeier–Haack Reaction
Capabilities for aldehyde and ketone group introduction into aromatic systems with efficient POCl₃ recovery and recycling processes.
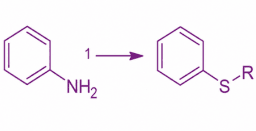
Thiolation
Experience in sulfur chemistry using thiourea, sodium polysulfides, and mercaptans across scalable manufacturing processes. Scale: 800 MT Year: 2004
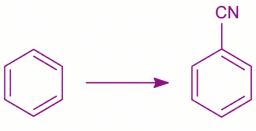
Cyanation
Capabilities for halogen replacement and nitrile synthesis with dedicated waste handling and process safety systems.
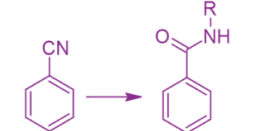
Ritter Reaction
Scalable amino group introduction capabilities for multi-step chemical synthesis applications.
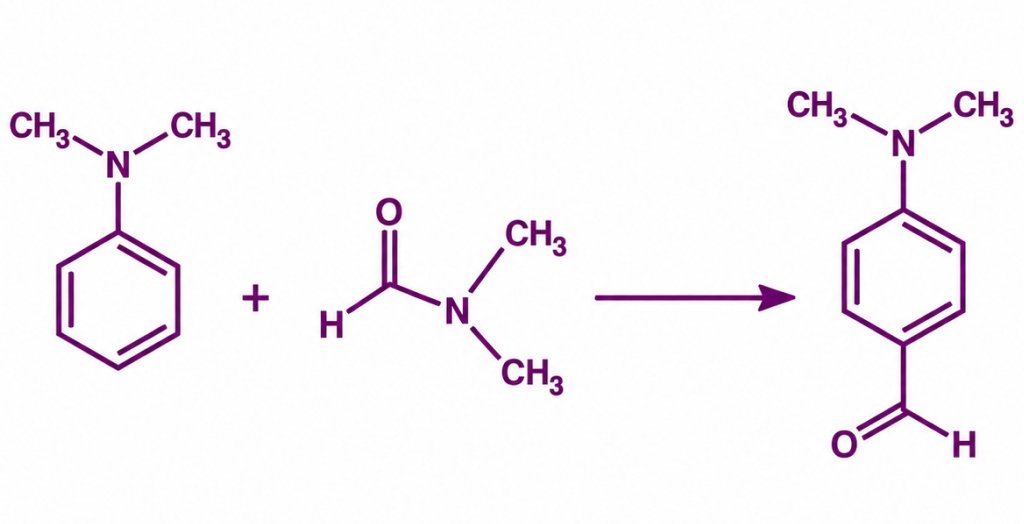
Diazotization & Sandmeyer Reaction
Expertise in halogen introduction, coupling reactions, keto compound synthesis, and alkyl thiol transformations. Scale: 1000 MT Year: 2017
O, C & N Alkylations
Capabilities across aliphatic, aromatic, and heterocyclic alkylation processes using diverse alkylating agents.
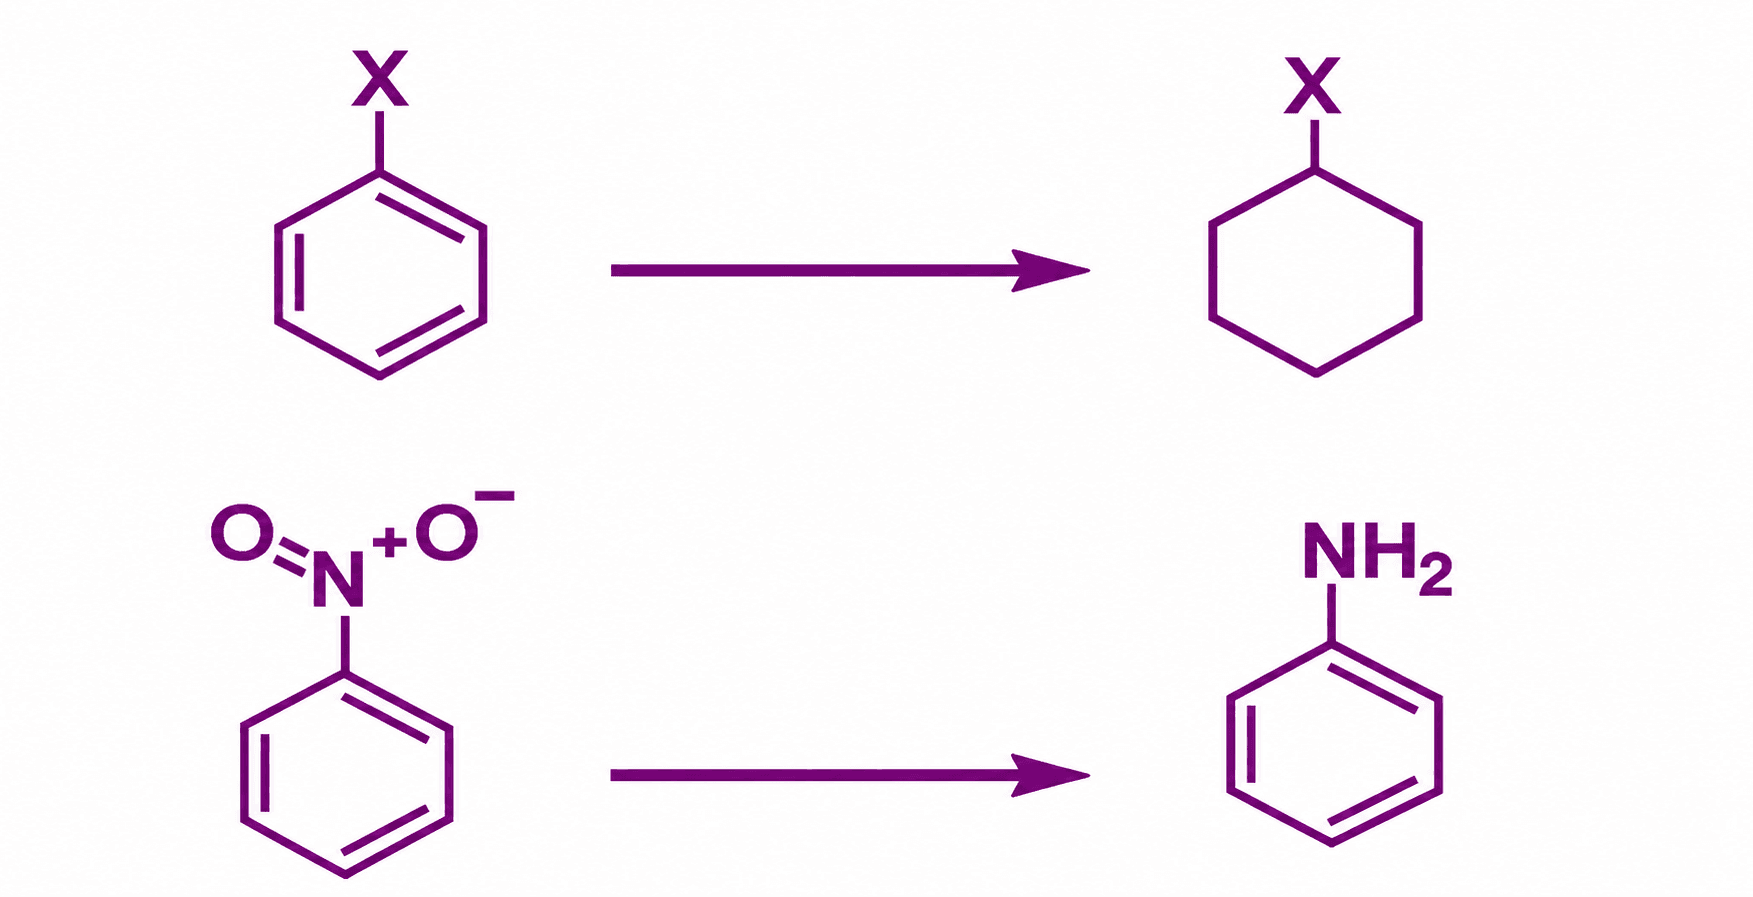
Hydrogenation
Commercial-scale hydrogenation capabilities for ring hydrogenation, nitro reduction, nitrile reduction, dehalogenation, and related high-pressure transformations using precious metal catalysts. Scale: 1500 MT Year: 2002
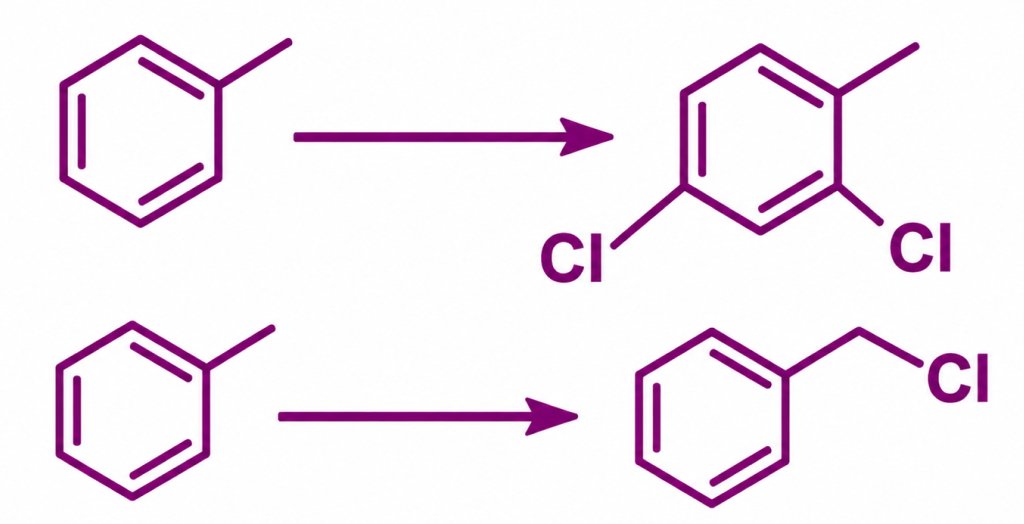
Chlorination
Expertise in chlorination using Cl₂, POCl₃, PCl₃, SOCl₂, SO₂Cl₂, and free radical chlorination processes with by-product recovery capabilities. Scale: 2000 MT Year: 2002
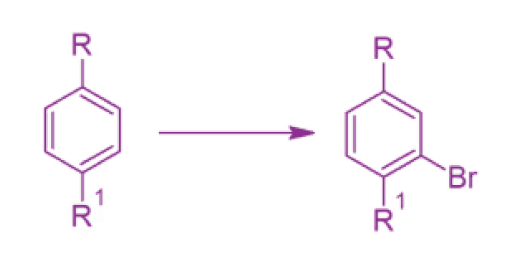
Bromination
Capabilities using bromine, aqueous HBr, and HBr in acetic acid with continuous bromine recovery and in-situ bromine generation systems. Scale: 500 MT Year 2015
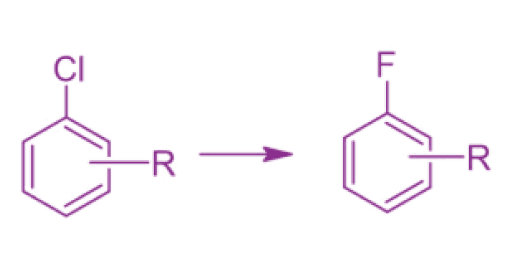
Fluorination
Capabilities across Halex fluorination, HF-based fluorination, and vapor-phase fluorination in fluidized bed reactors with advanced solvent recovery and recycling systems. Scale: 1200 MT Year: 2022
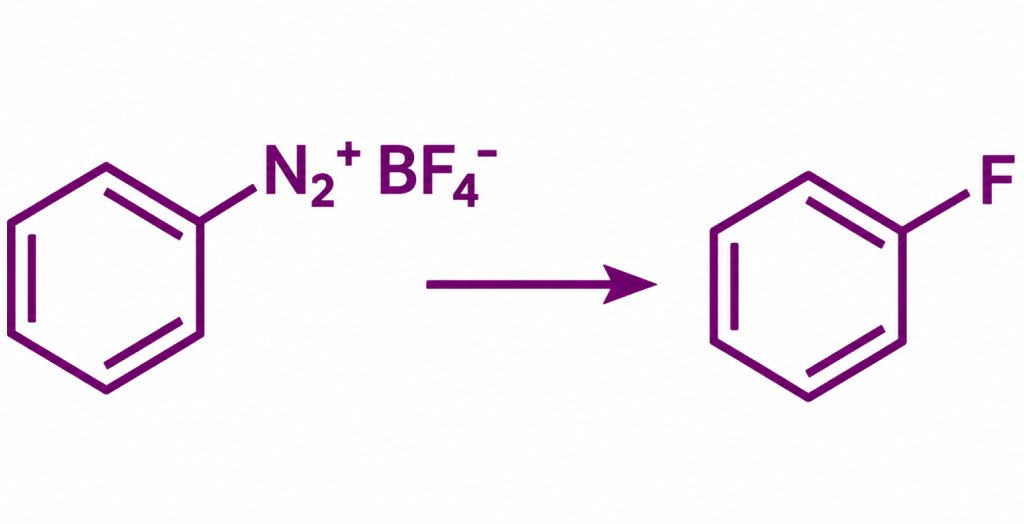
Balz-Schiemann Reaction
Lab-scale expertise in fluorination chemistry with BF₃ recycling capabilities.
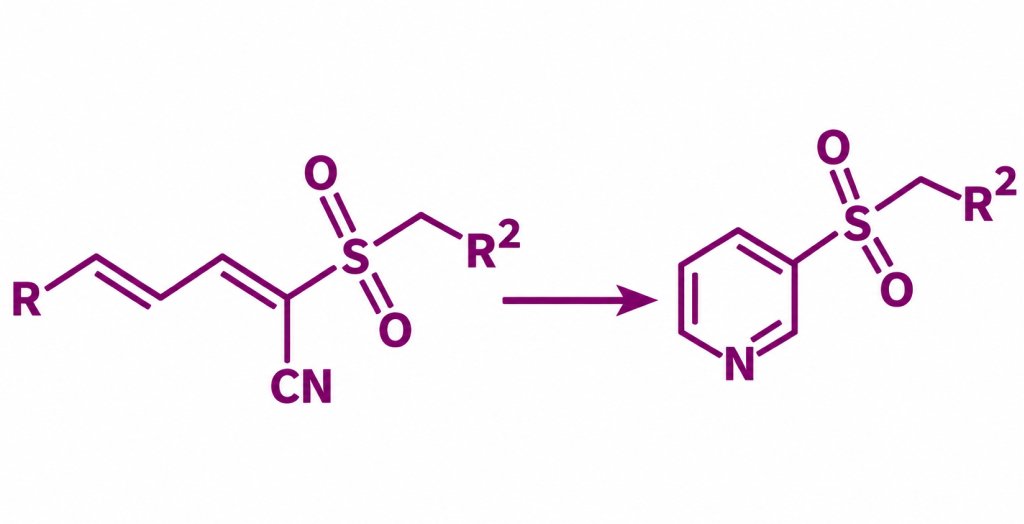
Heterocyclic Ring Formation
Expertise in synthesizing pyridine, pyrimidine, pyrazole, and related heterocyclic compounds using hydrazine-based chemistries.
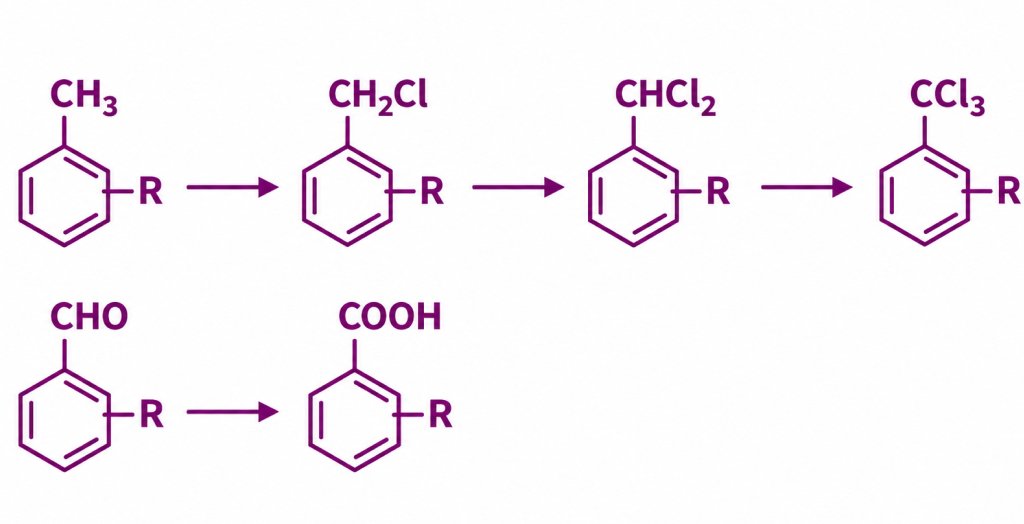
Photochlorination
Lab-scale expertise across aromatic and heterocyclic substrates with future pilot-scale scale-up capabilities.