
HomecapabilitiesManufacturing Infrastructure
Manufacturing Infrastructure
Overview
At Cohizon Life Sciences’ Ankleshwar sites, we have state-of-the-art chemical manufacturing sites designed for multi-step synthesis and commercial-scale production of agrochemical active ingredients, intermediates, building blocks, and non-GMP products. Advanced utilities, DCS-operated systems, hydrogen stations, and robust safety controls support complex and hazardous chemistries. Over two decades, Cohizon has continuously expanded its chemistry capabilities, beginning with nitration (75 MT) and amination (500 MT) in 1997, followed by hydrogenation (1,500 MT) and chlorination (2,000 MT) in 2002. In 2003, the company added heterocyclic ring formation & Vilsmeier (1,500 MT) and coupling reactions (700 MT), followed by sulfur chemistry/thiolation (800 MT) in 2004 and Friedel-Crafts (1,000 MT) in 2006. Further expansion included acid chloride formation (1,000 MT) in 2009, amidation (60 MT) in 2012, bromination (500 MT) in 2015, diazotization & Sandmeyer (1,000 MT) in 2017, hydrazine chemistry (80 MT) in 2021, and continuous vapor-phase fluorination / Halex (1,200 MT) in 2022. Today, Cohizon brings these capabilities together to deliver scalable, safe, and quality-driven commercial manufacturing across complex chemistries for agrochemical and specialty chemical applications.
Manufacturing Unit 1
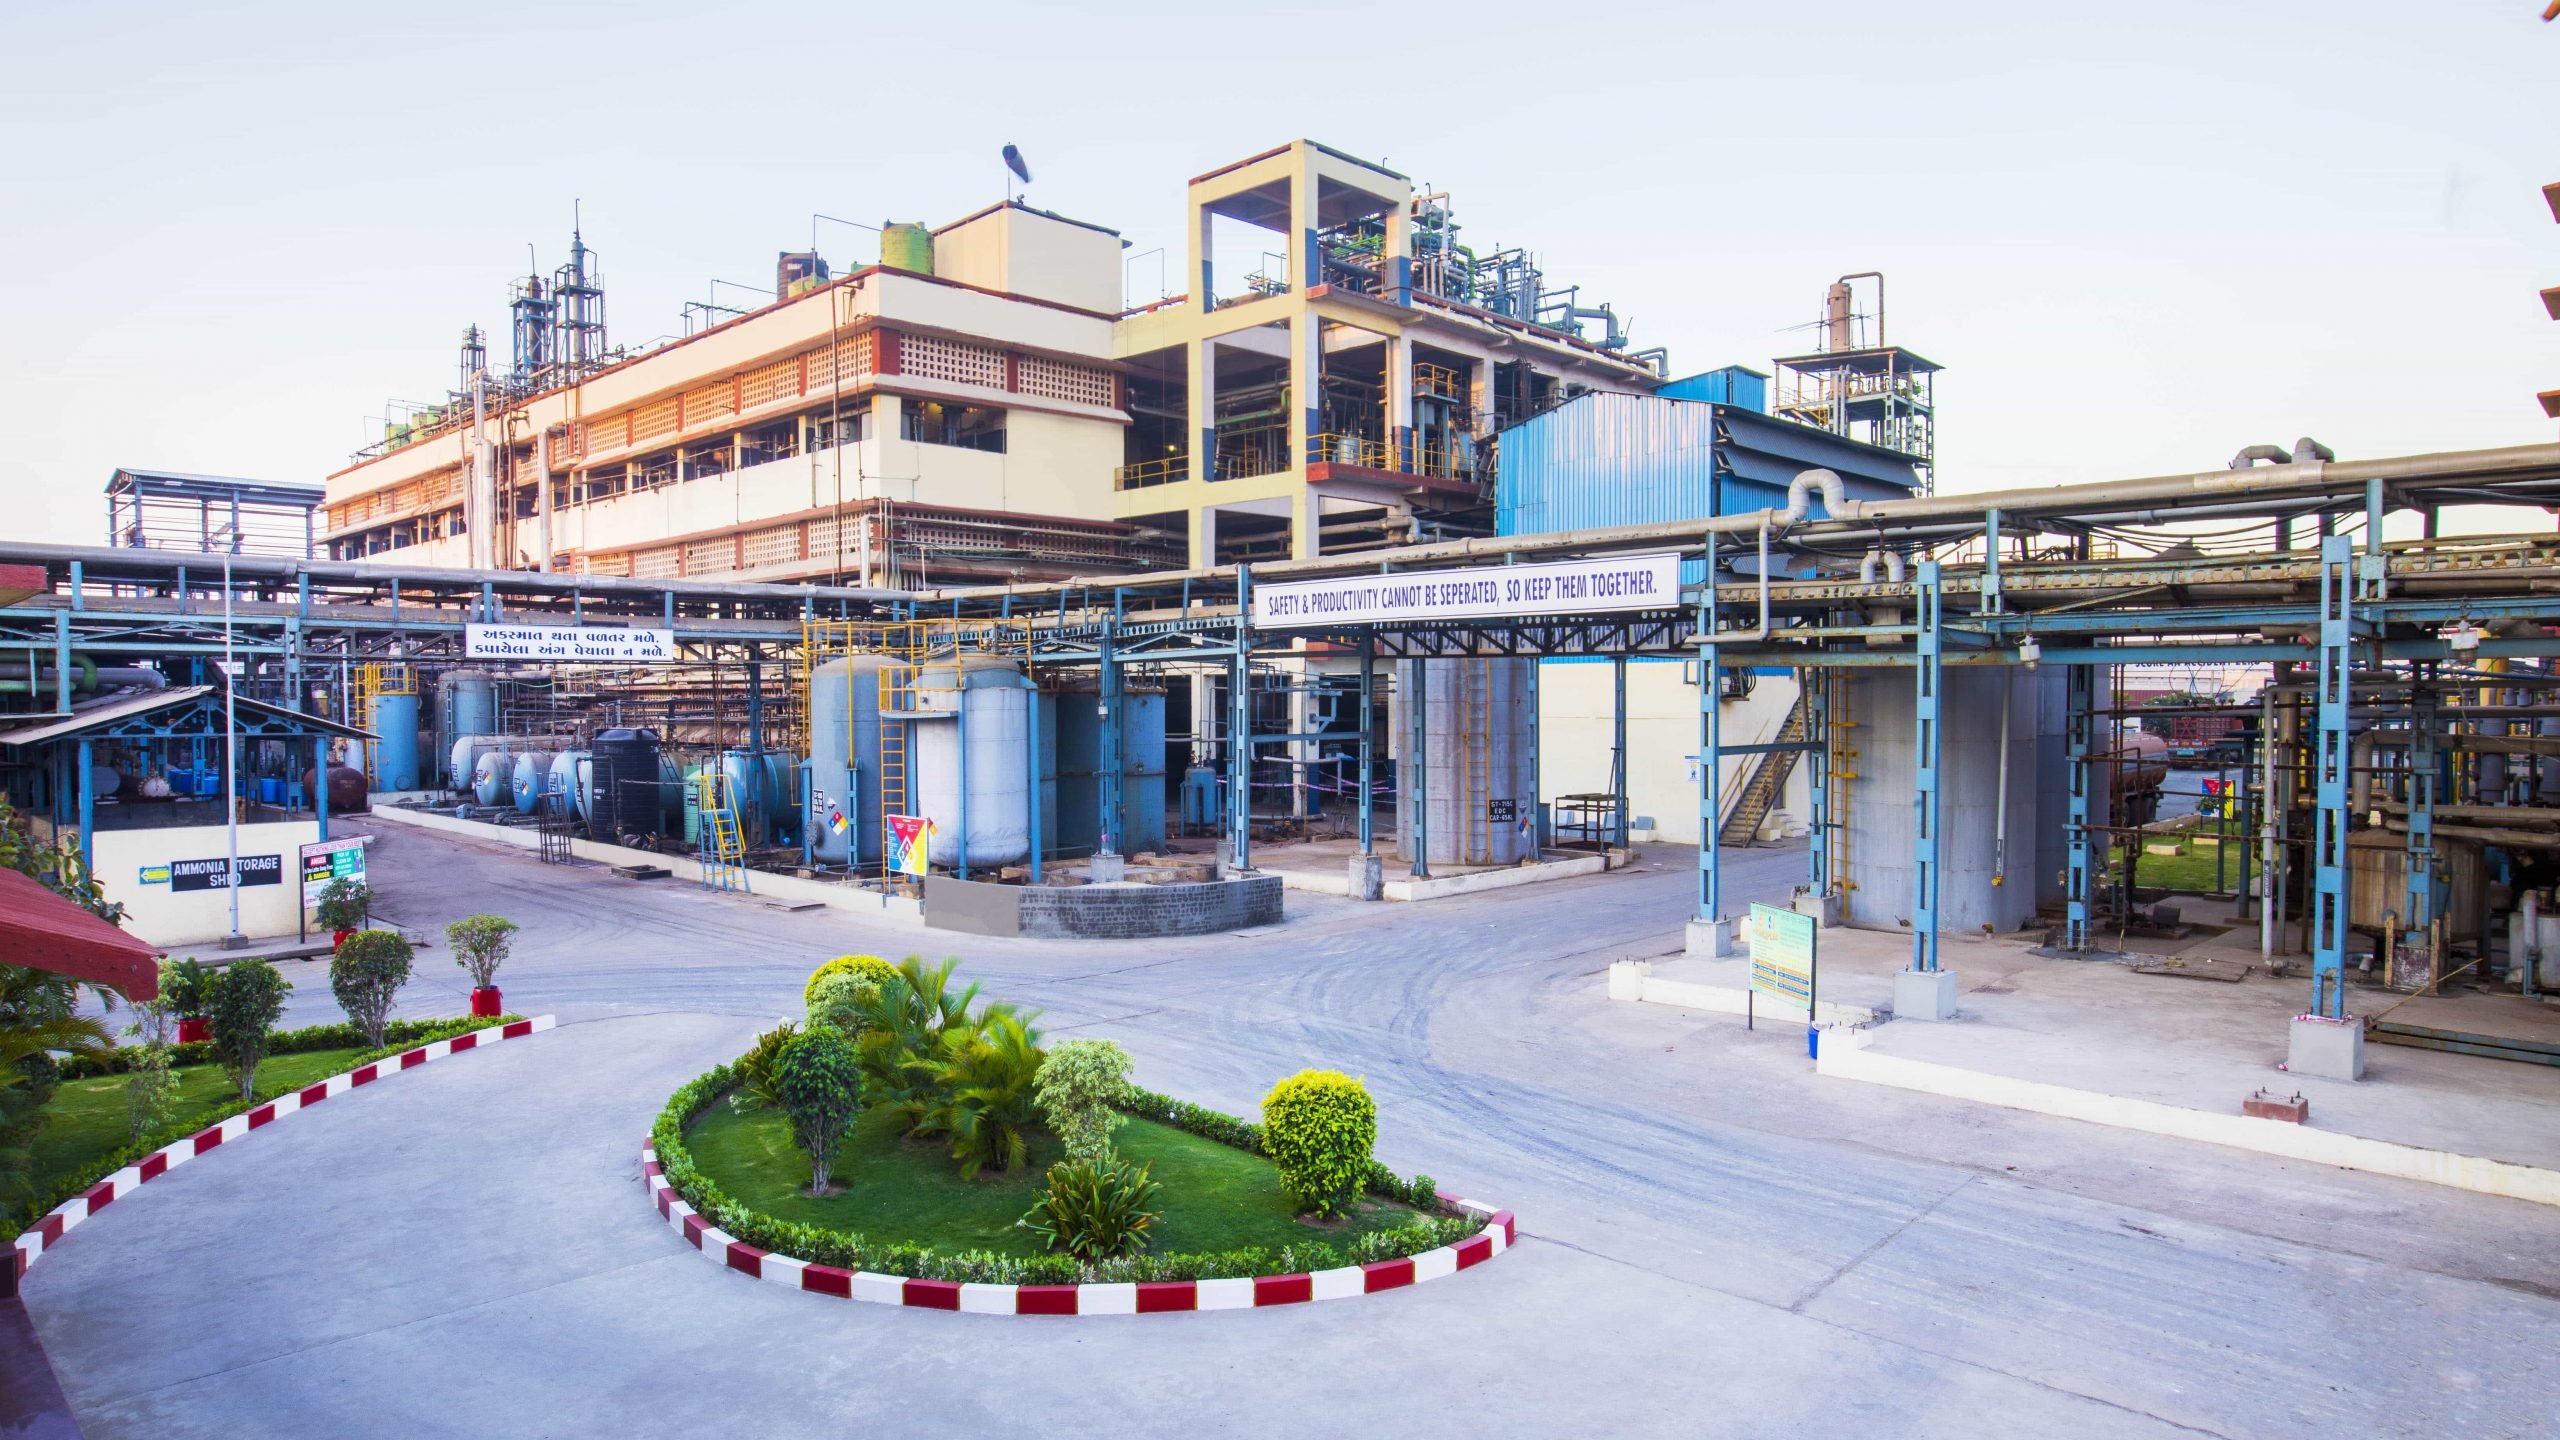
Our Manufacturing Unit 1 is an integrated manufacturing complex designed for multipurpose, commercial-scale chemical production. The site supports reaction scales from 1–25 KL with a total reactor volume of 2340 KL and more than 30 reaction capabilities, backed by advanced DCS-operated production infrastructure. Spread across 71,362 m² with a built-up area of 35,000 m², the facility includes five dedicated manufacturing plants, RM & FG warehouse infrastructure, a hydrogen station, utility and admin blocks, incinerator, MEE plant, dedicated ETP, brine & chilling plant, tank farm, and hazardous waste management facilities to support safe and efficient operations.
Agro, Non-GMP Pharma & Specialty Intermediates
Core Chemistries:
Amidation
Cyclization
Oxidative Chlorination
Diazotization
Sulfonamide Reaction
Bromination
Thiolation
Condensation

07
Product Streams

4000
TPA Capacity

87
Reactors (1090 KL)
Scale-Up
Journey
R&D
Develop robust and scalable processes.
Kilo Lab
Optimize reactions at kilogram scale.
Pilot Lab
Validate processes for manufacturing.
Scale-Up
Deliver consistent large-scale production.